0755-27781532-8010; 02988446863
Nov 09, 2026
PCBA Functional Testing: Procedures for Reliable Assemblies
Nov 17
Intelligent Browse: 1
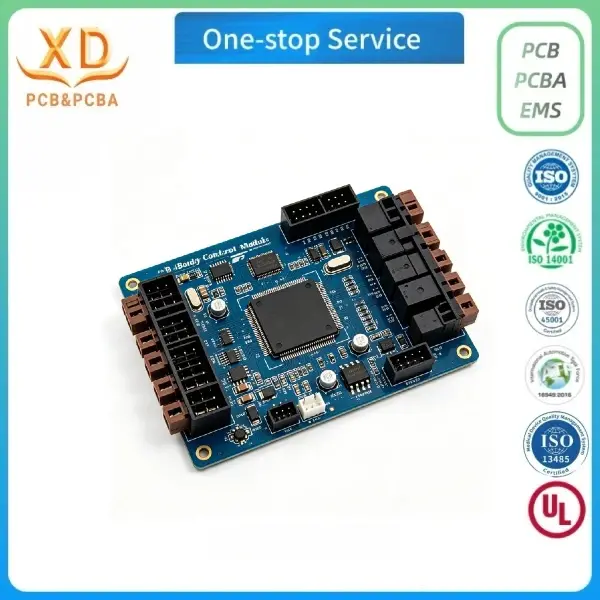
A printed circuit board assembly (PCBA) can pass visual inspection and still fail to perform its intended function. Incorrect component values, weak electrical connections, programming errors, interface problems or unexpected interactions between circuit sections may only become apparent when the assembled board is powered and operated. PCBA functional testing addresses this gap by checking whether an assembly performs the operations required by its design.
For electronics manufacturers, functional testing is an important part of production quality control. It evaluates the assembled board under defined operating conditions and helps identify failures that may not be detected through appearance checks alone. The test method, fixture, software, input signals and pass/fail criteria all need to reflect the product's actual requirements.
A well-planned process begins during product development, not after the first production batch has been assembled. Test access, programming interfaces, connector arrangements and measurable output signals should be considered during PCB design. This coordination helps make testing more repeatable as a project moves from prototype builds to volume production.
Shenzhen Xindaxing Electronics lists function testing among its EMS service items. For OEM and ODM projects, the test scope should be defined according to the circuit design, product application and customer acceptance requirements.
What Is PCBA Functional Testing?
PCBA functional testing is a process used to verify whether an assembled circuit board performs its intended electrical and operational functions. A test setup supplies defined inputs, monitors selected outputs and checks whether the board responds according to established requirements.
The test may involve applying power, sending commands, activating inputs, measuring signals, checking communication interfaces or observing output behavior. The exact procedure depends on the product. A simple control board may require only a limited set of input and output checks, while a more complex electronic assembly may need multiple operating modes and communication tests.
Functional testing differs from a basic electrical continuity check. Continuity testing can help identify open or short connections, but it does not necessarily confirm that the controller executes the correct logic, that an interface communicates properly or that an output responds to a command. Functional testing examines the board as an operating electronic assembly.
Functional Testing and Other PCBA Inspection Methods
Different inspection and test methods identify different types of defects. They should be selected according to the board's construction, component packages, circuit complexity and product risks.
| Method | Main purpose | Typical focus |
|---|---|---|
| Visual inspection | Checks visible assembly conditions | Component presence, orientation and obvious workmanship issues |
| AOI | Uses optical imaging to inspect assembly features | Soldering appearance, placement and visible defects |
| X-ray inspection | Examines internal solder connections that are difficult to view externally | Hidden joints, such as certain BGA connections |
| In-circuit testing (ICT) | Checks selected electrical characteristics at circuit nodes | Component values, shorts, opens and electrical connections |
| Flying probe testing | Uses movable probes to access test points | Electrical checks without a dedicated bed-of-nails fixture |
| Functional testing (FCT) | Checks whether the assembled board performs specified operations | Inputs, outputs, interfaces, control behavior and operating functions |
These methods are complementary rather than interchangeable. AOI and X-ray inspection focus on assembly conditions, while ICT and flying probe testing evaluate selected electrical characteristics. FCT checks the behavior of the assembled circuit under defined operating conditions.
A project does not automatically require every method. The appropriate test plan depends on the product's complexity, risk level, production volume, available test access and customer requirements.
Why PCBA Functional Testing Matters in Electronics Manufacturing
The purpose of functional testing is not simply to label a board as pass or fail. It provides evidence that the assembly can perform the functions defined for it and helps manufacturers identify defects before boards move to the next production stage.
Detecting Functional Defects After Assembly
Some defects are difficult to identify through visual inspection alone. A component may be installed in the correct position but have an incorrect value. A connection may appear acceptable while producing an intermittent signal. A controller may power on but fail to execute a required operation.
Functional testing can help identify problems such as:
Incorrect or missing output signals
Failure to respond to control inputs
Communication errors between circuit sections
Incorrect voltage or current behavior under defined conditions
Programming or configuration problems
Unexpected startup or reset behavior
Failure of a connected sensor, display or actuator interface
The test program should be designed around the board's actual functions. A generic power-on check is not sufficient when the product requires several operating modes, communication channels or controlled outputs.
Reducing the Risk of Defective Boards Reaching Later Stages
A failed PCBA may create additional costs if it is discovered only after enclosure installation, cable connection or final product assembly. Early testing helps separate board-level defects from problems introduced during later integration.
For example, a controller board used in an industrial device may need to communicate with an external display or sensor. If the communication interface is not tested before integration, a faulty board may be assembled into a larger unit before the issue is found. A defined PCBA test stage can identify the failure closer to its source.
The economic value depends on the production process and defect type. Functional testing does not eliminate all failures, but it can reduce the chance that detectable board-level problems continue unnoticed through manufacturing.
Supporting Consistent Production Quality
A repeatable test procedure provides a common basis for evaluating assemblies across production batches. When the same input conditions, test sequence and acceptance criteria are used, results become easier to compare.
Test records can also help identify recurring issues. A sudden increase in failures on one test step may indicate a component lot issue, an assembly process change, a programming mismatch or a problem with the test fixture itself.
The value of these records depends on their accuracy and traceability. A useful test record should identify the board or production lot, test program revision, result and relevant failure information.
PCBA Functional Testing Procedures
A reliable test process should follow a documented sequence. The steps below provide a general framework, but the actual procedure must be adapted to the circuit and product requirements.
Step 1: Review the Design and Define Test Requirements
The first step is to identify what the PCBA must do. Engineers should review the schematic, BOM, PCB layout, interface definitions, firmware requirements and product specifications.
The review should identify:
Required power inputs and operating ranges
Important signals and measurable test points
Expected input and output behavior
Communication interfaces and protocols
Startup, shutdown and reset conditions
Operating modes that need verification
Customer-defined acceptance criteria
Each requirement should be linked to one or more test steps. This creates a clear relationship between the product specification and the production test procedure.
If a requirement cannot be measured directly at the board level, the team should decide whether an indirect measurement or a higher-level product test is needed. This distinction prevents the PCBA test from being expected to verify functions that depend on external components or the complete product system.
Step 2: Prepare the Test Fixture and Equipment
A functional test fixture connects the PCBA to the equipment or system used to supply inputs and measure outputs. Depending on the board, it may include connectors, probes, cables, a power supply, communication interfaces, sensors, electronic loads or other test instruments.
The fixture should hold the board securely and provide repeatable electrical connections. Poor contact can create intermittent failures that are unrelated to the assembly itself. Mechanical alignment, connector durability and access to test points therefore matter.
Before the fixture is released for production, it should be checked with a known-good board or an approved reference unit. This helps confirm that the fixture, wiring and test software operate as expected.
The fixture design should also consider operator safety. Exposed power connections, high-voltage sections, moving mechanisms and stored energy require suitable safeguards based on the product's electrical characteristics.
Step 3: Establish the Test Program and Operating Conditions
The test program controls the sequence of operations and evaluates the measured results. It may instruct the board to enter a specific mode, send commands, read communication responses or activate outputs.
The program should define:
Test sequence and timing
Input values and signal conditions
Expected output ranges or responses
Communication commands and response criteria
Measurement limits and tolerances
Pass/fail rules
Error messages and failure codes
Test conditions must be consistent with the product specification. A voltage limit, timing requirement or communication response should not be selected simply because it produces convenient results. It needs to be supported by engineering requirements or approved customer criteria.
Program revision control is also important. If firmware or circuit behavior changes, the test program may need corresponding updates. The production team should be able to identify which test program revision was used for each batch.
Step 4: Perform Power-On and Basic Electrical Checks
Before running the full functional sequence, the board should be checked under controlled power conditions. This may include confirming supply voltage, observing current consumption and checking whether the board starts correctly.
Initial power-on testing should follow a safe procedure. Where the design has multiple power rails or high-current sections, the test sequence should account for their startup requirements and potential fault conditions.
Abnormal current consumption, unexpected heating, repeated resets or missing supply rails may indicate a problem that should be investigated before continuing. The test procedure should define when the board must be stopped rather than allowing a potentially damaged assembly to proceed through the remaining steps.
Step 5: Verify Inputs, Outputs and Interfaces
The main functional checks should cover the board's specified inputs and outputs. Test equipment can apply defined signals or commands and measure the corresponding response.
Depending on the product, this may include:
Digital input and output states
Analog signal measurement
Sensor input response
Relay or driver output behavior
Display or indicator operation
Serial communication
Wired or wireless interface response
Control signals between circuit sections
Each check should have an expected result and a defined acceptance range. For example, a test may verify that an output changes state after a specified command or that a communication interface returns the expected response.
Testing should also account for operating modes. A board that works in its default state may still fail when switching between modes, recovering from a reset or responding to an abnormal input.
Step 6: Record Results and Separate Failed Assemblies
The test system should record whether each required step passed or failed. For failed boards, the record should identify the test item and provide enough information to support investigation.
Failed assemblies should be separated from accepted products according to the production process. They should not be returned to the normal production flow until the issue has been reviewed and the required retest or approval has been completed.
A clear failure-handling process reduces the risk of accidental shipment and makes defect analysis more efficient.
Designing an Effective Functional Test Fixture for PCB Assembly
The test fixture has a direct influence on test repeatability. Even a well-written test program can produce unreliable results if electrical contacts are unstable, the board is positioned incorrectly or the fixture does not reproduce the required operating conditions.
Test Point Planning and Board Accessibility
Test access should be considered during PCB design. Engineers should identify which signals need to be measured and whether suitable test points, connectors or programming interfaces are available.
Test points should be positioned so that probes or fixture contacts can reach them reliably. Their size, spacing and location need to account for the board's component layout and the intended test method.
If test access is considered only after the PCB has been completed, the fixture may become more complicated. In some cases, additional adapters or manual connections may be required, increasing setup time and the possibility of operator error.
Electrical Connection and Mechanical Positioning
A fixture must maintain stable connections throughout the test sequence. Board supports, locating features and contact mechanisms should prevent unnecessary movement while avoiding excessive pressure on components or solder joints.
The fixture should also accommodate the board's approved revision and dimensions. If a design change affects connector position, board outline or test-point location, the fixture may need to be reviewed before the revised assembly enters production.
For projects with multiple board variants, clear identification and mistake-proofing measures can help prevent the wrong test setup from being used.
Test Software, Calibration and Reference Boards
Test software should use controlled versions and documented limits. Changes to measurement thresholds, timing or command sequences should be reviewed before release.
Measurement equipment may require calibration according to its use and applicable quality procedures. The test team should also establish checks for the fixture itself, since worn contacts, damaged cables or unstable power supplies can create misleading results.
A known-good reference board can help verify the test setup at defined intervals. However, it should not replace equipment maintenance or calibration. Reference-board checks, fixture inspection and program control serve different purposes and should be managed together.
PCBA Test Coverage and Pass/Fail Criteria
Test coverage describes how well the planned test process evaluates the functions and risks identified for a board. High test coverage does not simply mean running a large number of test steps. It means selecting tests that provide meaningful evidence about the assembly's required behavior.
Mapping Product Requirements to Test Items
A practical approach is to create a requirement-to-test matrix. Each important product requirement should be linked to a test method, expected result and acceptance criterion.
| Requirement area | Example test item | Acceptance basis |
|---|---|---|
| Power input | Apply specified supply condition | Voltage and current within approved limits |
| Startup | Power-cycle the board | Startup sequence completes as specified |
| Control logic | Send defined commands | Correct state or output response |
| Communication | Exchange data through an interface | Expected response and data format |
| Sensor interface | Apply a known input condition | Measured or reported value within limits |
| Output driver | Activate a controlled output | Required output state or electrical response |
| Recovery behavior | Apply a defined reset or restart | Board returns to the specified operating state |
The table is illustrative. Actual test items and limits must come from the product's approved design and specification.
Setting Meaningful Pass/Fail Limits
A test limit should distinguish acceptable variation from a real defect. Limits that are too wide may allow faulty boards to pass, while limits that are unnecessarily narrow may reject acceptable assemblies.
Engineering teams should consider component tolerances, measurement accuracy, normal operating variation and product requirements when setting thresholds. Where appropriate, measurement uncertainty should be considered so that the test does not create false failures near a limit.
Pass/fail criteria should be documented and approved before production. Informal changes made by operators or production personnel can make results inconsistent and weaken the value of the test records.
Avoiding False Failures and Missed Defects
A failed test does not always mean the PCBA is defective. The cause may be an unstable fixture contact, incorrect test setup, outdated software or an input condition that was not applied correctly.
Likewise, a board passing a limited test sequence does not prove that every possible operating condition has been verified. The test plan should focus on the functions and failure risks that matter to the product.
When a failure occurs, the team should distinguish between a genuine board defect and a test-system problem. This prevents unnecessary rework and helps maintain confidence in the testing process.
Managing Functional Testing from Prototype to Mass Production
The test strategy should evolve as a project moves through development and production. A procedure suitable for an engineering sample may need additional controls when the same board is manufactured in larger quantities.
Prototype Testing and Engineering Validation
During prototype development, functional testing helps confirm that the assembled board behaves as intended. Engineers may use laboratory instruments, development software or manually connected test equipment while refining the test sequence.
Prototype testing should focus on verifying key functions and identifying design gaps. If an important signal cannot be accessed or a required operating state cannot be reproduced, the test method may need to be improved before production.
The findings should be documented. Design changes, firmware updates and test-program revisions should be tracked so that later builds can be evaluated against the correct requirements.
Pilot Production and Test Process Refinement
A pilot build provides an opportunity to evaluate the test process under more representative production conditions. The team can review fixture handling, test duration, operator instructions, connection reliability and failure reporting.
Repeated test failures should be analyzed rather than treated as isolated events. A cluster of failures at one test step may indicate a design issue, an assembly process problem or a fixture limitation.
The pilot stage is also a suitable time to confirm that test records contain the information needed for production traceability and customer review.
Production Testing and Result Traceability
During volume production, test procedures should be standardized. Operators need clear instructions for loading the board, connecting the fixture, starting the test and handling failed assemblies.
Production records may include board or batch identification, test date, program revision, test result and failure code. The required level of detail depends on customer requirements and the product's quality plan.
A controlled retest policy is important. Repeatedly running a failed board until it passes can hide intermittent problems and make the recorded result misleading. Retesting should follow an approved procedure, with the original failure and subsequent result retained where traceability is required.
Common Challenges in PCBA Functional Testing
Even a carefully designed test plan can encounter practical problems. Recognizing common issues helps engineering and manufacturing teams improve the process.
Incomplete Test Requirements
If the product requirements are unclear, the test program may cover only basic power-on behavior while missing important operating functions. Before fixture development, the engineering team should confirm the required inputs, outputs, modes, interfaces and acceptance criteria.
Limited Test Access on the PCB
Insufficient test points or poorly positioned connectors can make automated testing difficult. This issue is best addressed during PCB layout review, before the board design is released for fabrication.
Unstable Fixture Connections
Worn probes, loose connectors, contamination or poor board positioning can cause intermittent failures. Regular fixture checks and suitable maintenance procedures help distinguish test equipment issues from genuine PCBA defects.
Outdated Test Programs
A revised PCB or firmware version may change signal behavior or test requirements. If the test program is not updated and controlled, it may produce incorrect results. Design, firmware and test revisions should therefore be managed together.
Unclear Failure Analysis and Retest Rules
A pass/fail result is only the beginning of failure handling. Production teams need a process for isolating failed boards, recording symptoms, investigating root causes and approving rework or retest. Without these controls, the same defect may recur across multiple batches.
Choosing a PCBA Manufacturer with Functional Testing Capabilities
Functional testing should be considered when evaluating a PCBA manufacturing partner, especially when the board includes control logic, communication interfaces, sensors or product-specific operating functions.
A useful supplier review should cover several areas:
Test requirement review: Can the supplier review the schematic, BOM, interface information and customer test requirements before production?
Test fixture planning: Can the required fixture connections and test access be identified early?
Program and revision control: Are test programs and acceptance limits managed through defined revisions?
Failure handling: Is there a documented process for isolating failed boards and investigating test results?
Production records: Can test results be recorded according to the project's traceability requirements?
Engineering communication: Can the supplier coordinate with the customer when a test condition, limit or interface requirement needs clarification?
Customers should provide the latest approved design files, firmware information where relevant, interface specifications and test requirements. If a customer already has a functional test procedure or fixture, responsibilities for fixture ownership, maintenance, software updates and result records should be agreed before production begins.
A manufacturer should not be expected to infer product behavior from the PCB layout alone. Clear technical documentation makes it easier to establish a test process that reflects the intended application.
PCBA functional testing verifies whether an assembled circuit board performs the functions defined by its design. Effective testing depends on clear requirements, suitable test access, reliable fixtures, controlled test programs, meaningful pass/fail criteria and consistent failure handling. When these elements are considered during development, the test process can support both prototype validation and repeatable production quality control.
For OEM and ODM electronics projects, functional testing should be planned alongside PCB design, component sourcing and PCBA assembly. The test scope needs to reflect the board's actual functions rather than rely on a generic checklist. Shenzhen Xindaxing Electronics lists function testing as part of its EMS service offering. Companies planning a PCB assembly project can share their design files and testing requirements through the official Contact Us page to discuss the manufacturing and test arrangements.
Label: